G-CODE → 2026-09-26
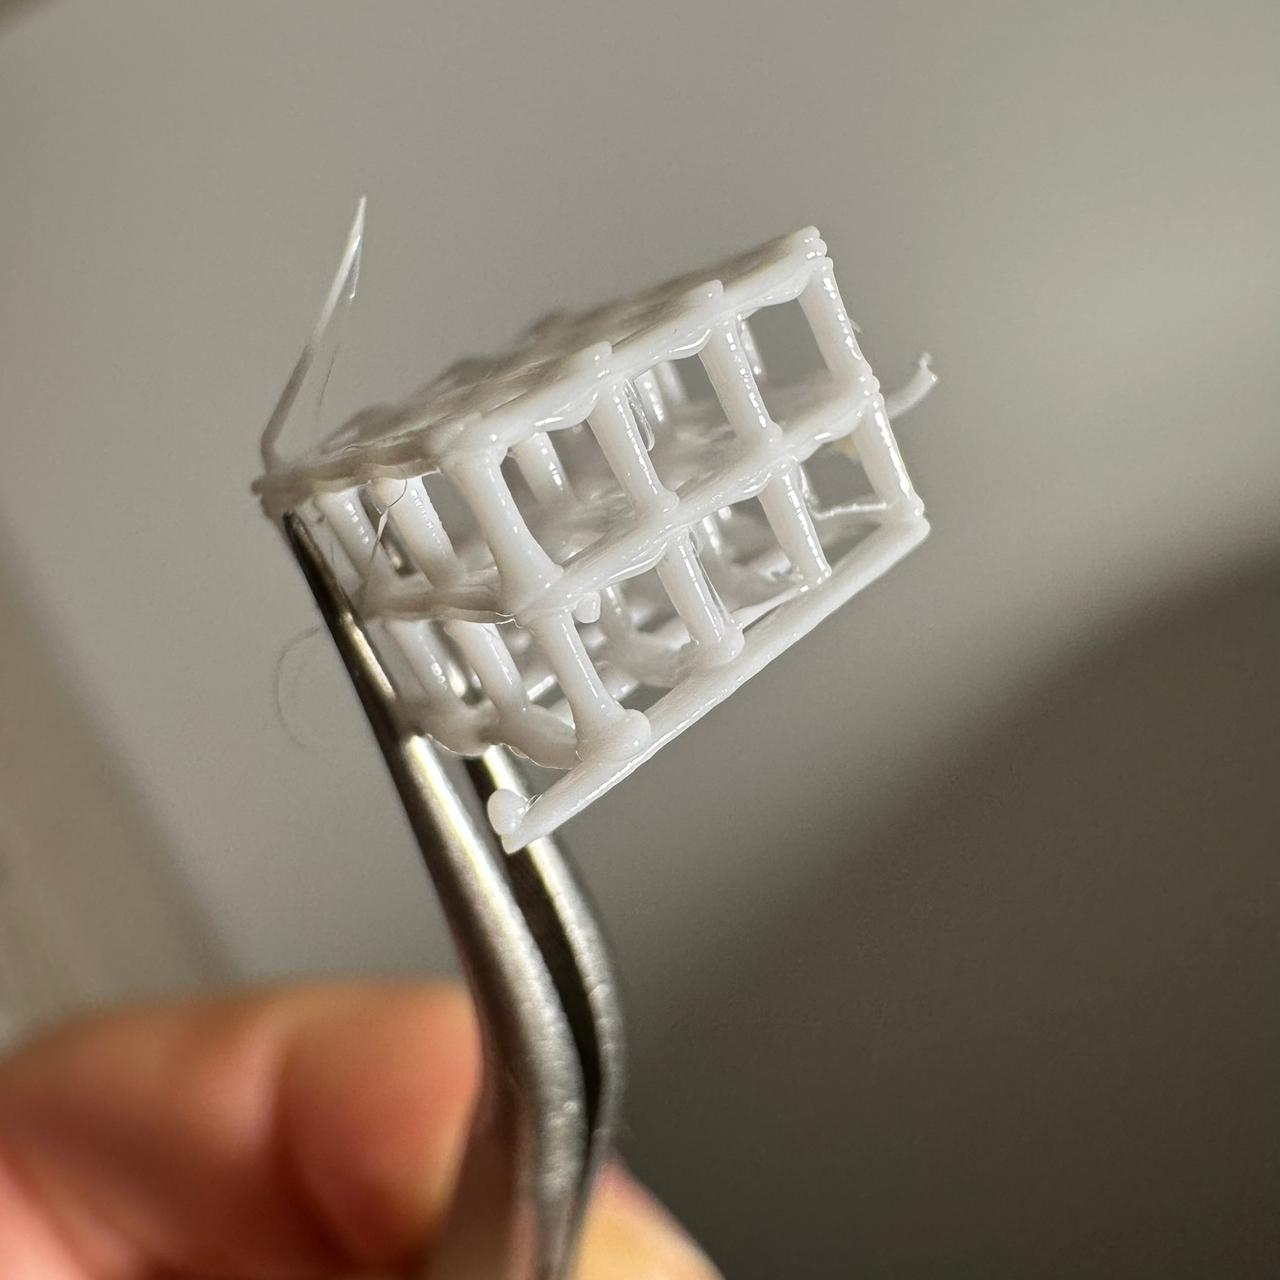
This is perfect. Well, perfect enough for now. I can print a larger one next.
Print parameters
Stem cube, straight travels — 2026-09-26 (sketch 2026.09.26 stem cube straight, commit 8395a88)
- Bambu Lab P1S, 0.4 mm nozzle, Textured PEI Plate
- Syntech PETG White, Ø1.75 mm, donor
_donor_3mf/L.gcode.3mf - Temperatures: nozzle at 235 °C throughout the print, including the bed grid (M109 wait before the grid); bed at 70 °C
- Part cooling at 100%
- Cube of 3 × 3 × 2 cells measuring 3 × 3 × 3 mm each: 4 × 4 nodes at 3 mm spacing, 9 × 9 mm footprint, centred at X128 Y128; top of the final beam at Z 6.7 mm (calculated)
- Bed grid: 4 rows at Z 0.5, 4 columns at Z 0.7, 0.8 × 0.5 mm line with 1.2 overfill (0.48 mm³/mm), 20 mm/s; the front-left corner is marked with a tail extending 5 mm left from the front line
- 2 tiers at 3 mm each: 2.4 mm stem + 0.6 mm beam (4 passes at 0.2 mm increments). Stem tops by tier at Z 3.1 / 6.1
- 16 stems per tier, 32 total; serpentine traversal from the front-left corner: one row left to right, the next right to left, rows front to back
- Each stem:
- Lower to the top of the node with no gap.
- Unretract 0.8 mm and pause for 0.5 s.
- Rise 2.4 mm while extruding 0.5 mm³ per millimetre of rise at 0.5 mm/s (calculated flow 0.25 mm³/s).
- Pause for 1.5 s at the top.
- Retract 0.8 mm, lift 1 mm above the tops, and travel to the next stem at 60 mm/s.
- Beams over the stem tops on each tier, 4 passes at 0.2 mm increments, with the first at stem-top height:
- Layer 1, rows — back to front from the left edge: 0.07 mm³/mm strand, with 0.2 mm³ pads at both ends of the first strand.
- Layer 1, columns — left to right from the front edge: 0.07 mm³/mm strand, with 0.2 mm³ pads at both ends of the first strand.
- Layer 2, rows — front to back from the right edge: 0.14 mm³/mm strand, with 0.2 mm³ pads at both ends of the first strand.
- Layer 2, columns — right to left from the back edge: 0.14 mm³/mm strand, with 0.2 mm³ pads at both ends of the first strand.
- Each beam line consists of two strands offset ±0.175 mm from the node axis (0.35 mm between strands), printed at 15 mm/s: outward along one strand, turn, then back along the other. Pads are extruded in place at 6 mm³/s
- Between beam lines: lift 0.5 mm, travel along the field edge at 60 mm/s, lower; no retraction
- Direct travels: except for the move from the start to the grid, each travel follows X or Y or includes a 0.175 mm offset on the second axis (at a field corner when switching beam passes and from the last beam of a tier to the first stem of the next tier)
- Print time 4 min 32 s, filament 62 mm