G-CODE → 2026-09-26
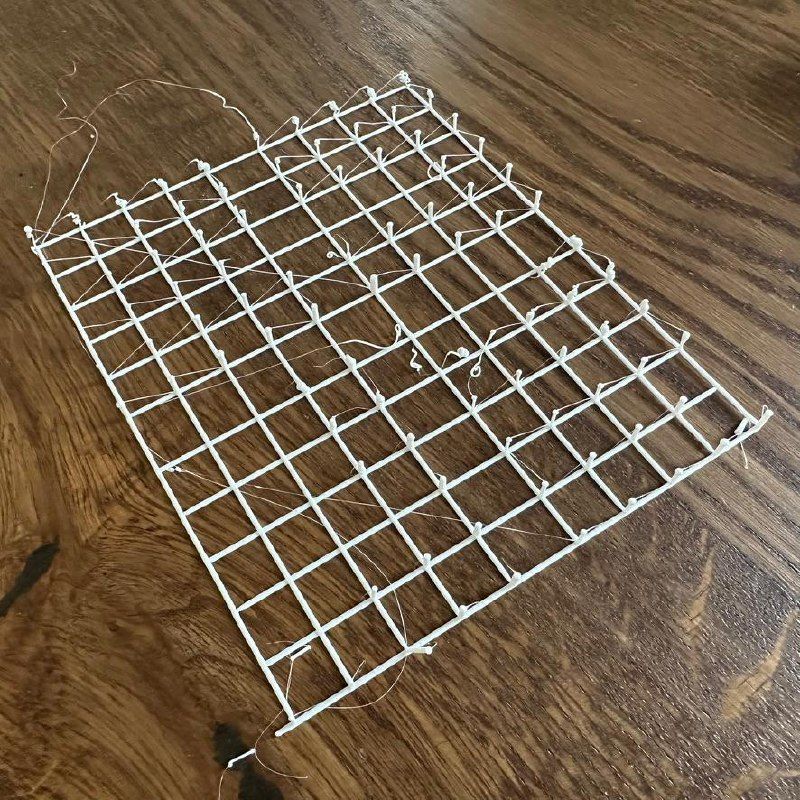
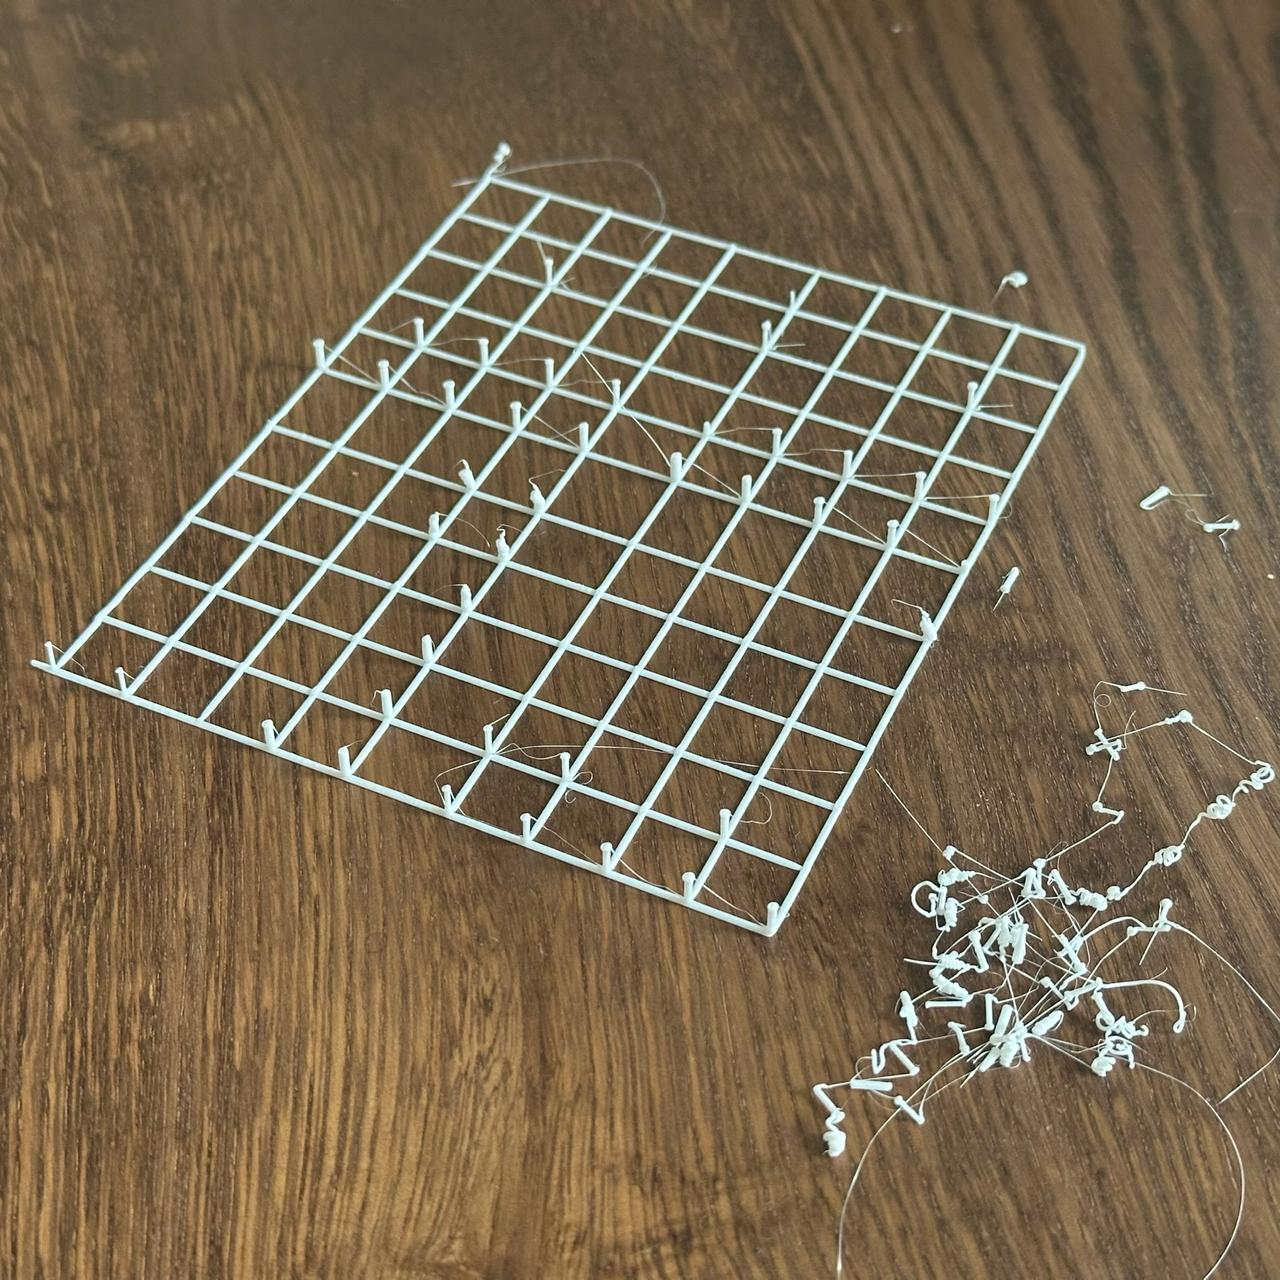
I tried to find suitable parameters for printing a stem. The test piece has four temperature zones, each with a 5 × 6 array of stems.
Within each zone, thickness changes from left to right (thicker on the right), while extrusion speed changes from bottom to top (faster at the top).
In the second photo, I snapped off the stems that came away easily.
For some reason, the thin stems in the first columns become thick, apparently because of the long pause. The pause is there to let the nozzle heat the filament. Some columns have caps on top: this is plastic oozing during the pause.
The stems need to be extruded slowly: only the bottom two rows came out properly. The fine string breaks only at the lowest temperature; at the other temperatures it reaches all the way down to the base.
Print parameters
Stem probe — 2026-09-25 (sketch 2026.09.25 stem probe, commit 8c2a9b4)
- Bambu Lab P1S, 0.4 mm nozzle, Textured PEI Plate
- Syntech PETG White, Ø1.75 mm, donor
_donor_3mf/L.gcode.3mf - Temperatures: nozzle at 255 °C for the base grid (the donor temperature), then 235 / 245 / 255 / 265 °C by block; bed at 70 °C
- Part cooling fan: 100%
- Four blocks in a 2 × 2 arrangement, each 48 × 60 mm, with a 16 mm gap between blocks, centered at X128 Y128; 235 °C front left, 245 °C front right, 255 °C rear left, 265 °C rear right
- One base grid shared by all blocks: rows at Z 0.5, columns at Z 0.7, 0.8 × 0.5 mm line with a 1.2 over-extrusion factor (0.48 mm³/mm), 20 mm/s; the front-left corner is marked by a tail, with the front line extending 5 mm left beyond the field
- Parameter grid: along X, extrusion 0.2 / 0.5 / 0.8 / 1.1 / 1.4 mm³ per mm of upward travel; along Y (front to back), upward speed 0.25 / 0.5 / 1 / 2 / 4 / 8 mm/s
- Stem spacing 12 mm, 30 stems per block, 120 total
- Each stem:
- Descend to Z 0.7, directly to the base-grid node with no gap.
- Unretract 0.8 mm; there is no separate base.
- Rise to Z 5.7, a 5 mm move with the column’s extrusion rate and the row’s speed.
- Pause for 1.5 s at the top.
- Travel moves: retract 0.8 mm, lift 1 mm above the stem tips, travel at 60 mm/s, descend, unretract 0.8 mm
- Order: print the entire base grid at the donor temperature, then print the blocks from coldest to hottest while waiting for each target temperature (M109); within each block, print the stems in a snake pattern, with even rows left to right and odd rows right to left
- Peak flow 11.2 mm³/s, calculated for the 1.4 mm³/mm × 8 mm/s cell
- Print time: 19 min 15 s; filament: 740 mm
Generator — run.py.